
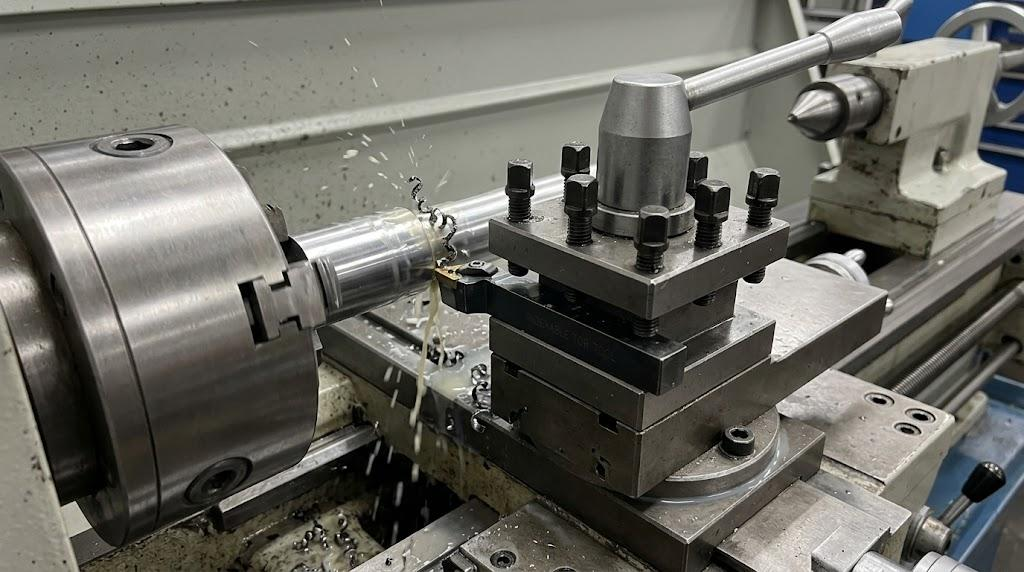
Hearing a squealing noise and seeing chatter marks on your metal part is frustrating. It ruins the surface and wastes good material. To fix lathe vibration quickly, you need to check three basic things: your tool overhang, how you hold the metal, and your spindle bearings.
1. Your Tool is Sticking Out Too Far
The most common reason for chatter is very simple: your cutting tool is sticking out too far from the tool holder.
Think about holding a heavy stick. If you hold it at the very end, your hand will shake. The same thing happens to your cutting tool. The pressure from the spinning metal makes the long tool bend and bounce.
The Fix: Keep the tool as short as possible. Push it deep into the tool post.
2. The Metal is Bending (Poor Clamping)
If you are cutting a long piece of metal, the chuck cannot hold it steady by itself. When the tool hits the metal, the free end of the metal gets pushed away. This bouncing creates ugly rings on your part.
This is especially true when you are doing heavy cuts on a conventional lathe . You need solid support on both ends.
The Fix: Always use a tailstock with a live center to hold the other end of long parts. If the part is very long, use a steady rest.
3. Loose Spindle Bearings
If your tool is short and your metal is held tight, the machine itself might be the problem.
Inside the machine head, the spindle spins on bearings. Over time, these bearings get a little loose. If there is too much space (clearance) inside, the whole spindle will shake when you start cutting. Our partner factory has been building machines since 2003, and we see this a lot in older repair shops.
The Fix: Check your manual and adjust the spindle bearing clearance. It should be tight enough to spin smoothly without any play.
Troubleshooting Cheat Sheet
Keep this simple chart near your machine to fix chatter fast:
| What You Hear/See | The Main Problem | How to Fix It Quickly |
|---|---|---|
| High-pitched squeal | Tool overhang is too long | Push the tool further back into the holder. |
| Rings on long parts | The metal is bending | Use a tailstock center to support the end. |
| Whole machine shakes | Spindle is loose | Adjust the spindle bearing clearance. |
Market Insight
Wasting metal is expensive. Many repair shops think a bad surface finish means they need to buy expensive new tools. But setting up the machine correctly the first time cuts down metal waste by a huge amount. A smooth cut saves material, saves time, and keeps your customers happy.
Need help finding the right machine for your shop? Contact our team anytime:
Email: info@mfg-machinery.com
Tell/Whatsapp: +86 175 2133 1995