
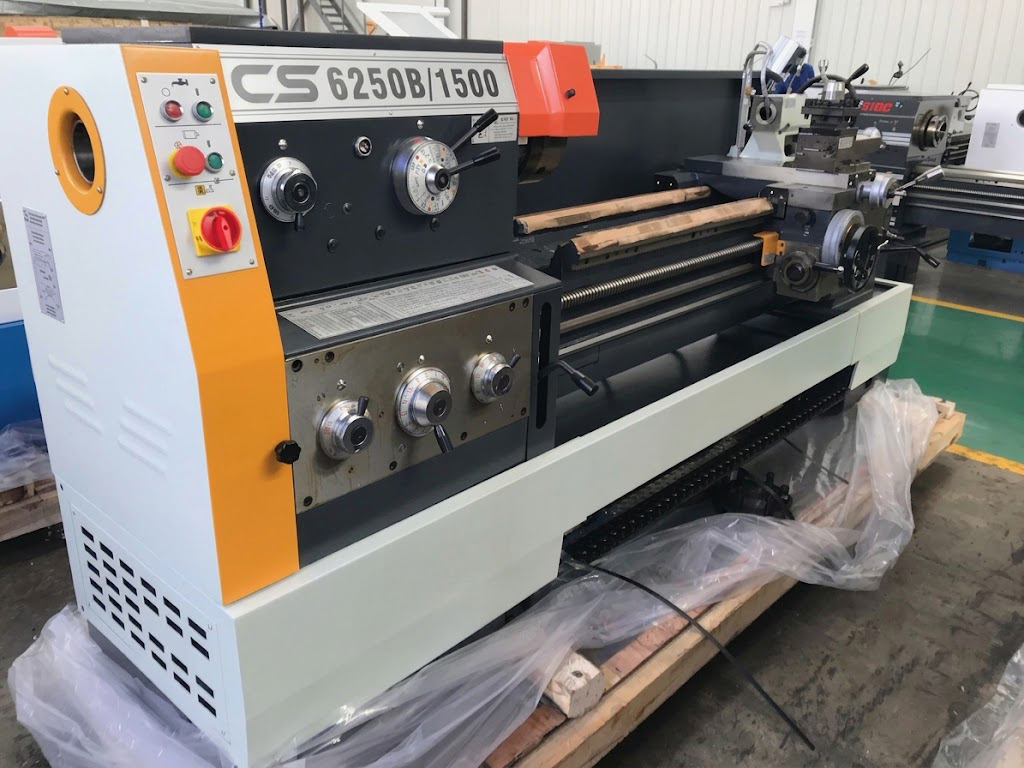
What methods can novice operators adopt to avoid tool chatter and tool chipping when working on the CS6250 conventional lathe?
Running a conventional lathe like the CS6250 requires a solid understanding of machine setup, tooling, and cutting parameters. Because the CS6250 features a sturdy cast-iron bed and high spindle torque, most chatter, vibration, and insert chipping issues stem from improper setup rather than machine limitations.
Follow this step-by-step practical guide to eliminate tool chipping, stop chatter marks, and achieve a smooth surface finish every time.
1. Understand Your CS6250 Lathe
The CS6250 is a mid-sized horizontal lathe ideal for rough and finish turning of steel, cast iron, and aluminum.
Strengths: Excellent rigidity for short, chunky shafts and flange parts.
Watch Out For: Long shafts and thin-walled parts are prone to vibration. Avoid extremely low RPM ranges (like 200–300 RPM) during heavy cuts, as they easily trigger machine resonance. Always check that your carriage gibs are properly adjusted to minimize play.
2. Tooling: The Key to Preventing Insert Chipping
Tool selection and installation are the most critical factors in stopping sudden insert breakage.
Insert Selection by Material
Carbon Steel (e.g., 45# Steel): Use YT5 for roughing and YT15 for finishing. Choose inserts with a negative land to increase impact resistance. Use an R0.8 nose radius for roughing and R0.4 for finishing (avoid delicate R0.2 tips for heavy cuts).
Stainless Steel: Use YW2 or YW3 grades with larger edge chamfers to reduce impact shocks. Never use standard carbon steel inserts on stainless steel.
Aluminum Alloys: Use sharp YG8 inserts to minimize cutting resistance and prevent material built-up edge (BUE).
Correct Tool Installation
Tool Height: Align the tool tip precisely with the workpiece centerline (within $\pm0.5$ mm). A high tool tip causes excessive squeezing and chipping; a low tool tip causes the tool to dig in and vibrate heavily.
Overhang: Keep tool overhang as short as possible (overhang $\le 3 \times$ tool shank thickness). Long overhangs reduce rigidity and trigger chatter instantly.
Clamping: Secure all clamping screws evenly using a diagonal pattern. Loose tools will shift mid-cut, destroying inserts and workpieces.
3. Workpiece Clamping: Eliminating 80% of Vibrations
Short Workpieces (Chucking): Ensure the gripping length is at least $1.5 \times$ the workpiece diameter. Clean the chuck jaws thoroughly to remove chips and burrs that cause slippage.
Long Shafts ($>300$ mm): You must use the tailstock center. Adjust the tailstock pressure properly: the workpiece should turn smoothly by hand without axial play. For slender shafts (length-to-diameter ratio $>20$), a steady rest is mandatory.
Thin-Walled Parts: Use soft jaw covers (like copper shims) to prevent clamping distortion. Keep cutting depths light to avoid spring-back vibration.
4. CS6250 Safe Cutting Parameters
Use these reliable, beginner-friendly parameters to ensure stable cutting without tool failure:
| Material | Operation | Spindle Speed (RPM) | Depth of Cut (ap) | Feed Rate (f) | Notes |
| 45# Steel | Roughing | 400 – 600 | 1.5 – 2.5 mm | 0.2 – 0.3 mm/rev | Avoid the 200–300 RPM resonance zone |
| 45# Steel | Semi-Finishing | 800 – 1000 | 0.3 – 0.8 mm | 0.1 – 0.15 mm/rev | Keep allowances even to minimize impact |
| 304 Stainless | Roughing | 250 – 350 | 1.0 – 1.8 mm | 0.15 – 0.2 mm/rev | Low speed and feed prevent tearing |
| Aluminum | Roughing | 1200 – 1600 | 2.0 – 3.0 mm | 0.25 – 0.35 mm/rev | High speed for fast, low-resistance cutting |
Beginner Red Lines: Never run heavy cuts below 100 RPM. Avoid feeding too fast, and always take a light skim pass on uneven forged or cast surfaces before ramping up the cutting depth.
5. Quick Machine Tune-Ups
Carriage Gibs: Adjust the top and cross-slide gibs so they move smoothly by hand with zero side-to-side play.
Spindle Belts: Ensure drive belts are properly tensioned to prevent slipping and speed fluctuations.
Lubrication: Keep guide rails well-lubricated to prevent stick-slip behavior and intermittent chatter marks.
6. Pro Operating Habits
Always start the spindle and let it reach full speed before feeding the tool into the workpiece. Never engage the workpiece while the spindle is stationary.
Always retract the tool clear of the cut before stopping the spindle.
Use plenty of coolant when machining steel and stainless steel to prevent thermal softening and rapid tool wear.
Need Expert Machining Support or Custom Tooling?
At MFG machinery Equipment, we specialize in providing high-performance cutting tools, reliable machine accessories, and expert technical consulting for conventional and CNC machining operations. Whether you need help optimizing your CS6250 parameters or sourcing durable carbide inserts, contact our engineering team today to boost your shop floor productivity and part quality!
Website: https://www.mfg-machinery.com/
Email: info@mfg-machinery.com
Phone:+86 17321191875