
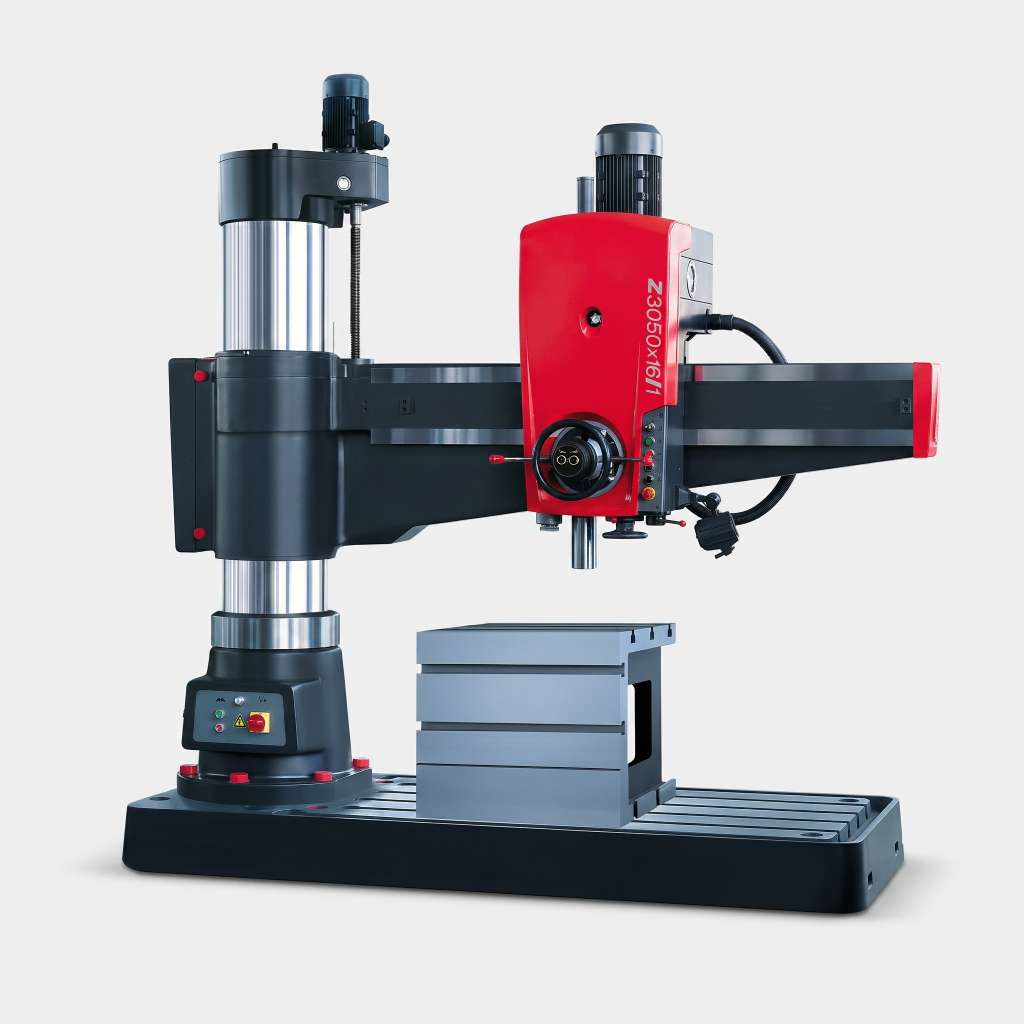
Achieving high-precision drilling, reaming, and boring (IT7-IT8 grade) on a radial drill machine requires overcoming inherent challenges like arm deflection, spindle clearance, and table rigidity. This guide breaks down the core strategy into five essential modules.
1. Machine Pre-processing: Eliminating Rigidity & Clearance(90% of precision loss stems from machine setup)
Sequential Locking: Always lock in this order: Column Clamp → Arm Saddle → Spindle Head. Locking only one part causes microscopic deflection.
Minimize Overhang: Keep the spindle sleeve extension ≤50mm. Use long carbide boring bars for deep holes to reduce sleeve exposure.
Thermal Stabilization: Run the spindle for 3-5 minutes to warm up. Before precision work, manually push-pull the spindle to eliminate gear backlash.
Worktable Leveling: Ensure table flatness/level is within 0.02mm/m. Use full-surface shimming to prevent workpiece distortion.
2. Tooling and Positioning
Fixture Strategy: For small batches, use a 0-grade precision vise with parallel bars. For high-volume production, use Drill Jigs with hardened tungsten carbide drill bushings (clearance ≤0.5D).
Clamping Technique: Align clamping points directly with support points. For thin-walled parts, perform a "roughing" clamp, release, and then "finish" clamp to relieve internal stress.
Tooling Accuracy: Clean all Morse tapers thoroughly. Avoid standard drill chucks for finish work; use integrated Morse taper tool holders to minimize radial runout.
3. Optimized Cutting Process
Follow the "Three-Step" process: Rough Drilling → Semi-finish Boring → Precision Reaming/Boring.
| Process Step | Goal | Key Strategy |
| Rough Drilling | Remove material | Use 118° symmetric split-point drill; leave 0.2-0.4mm for finish. |
| Semi-finish Boring | Correct alignment | Increase RPM by 20% compared to drilling; use light feed. |
| Finish Reaming | Surface finish | Use a Floating Reamer Holder to compensate for spindle tilt. |
| Finish Boring | Precision sizing | Use micro-adjustable boring bars; perform two-pass cuts. |
4. Advanced Operational Techniques
Pre-load Feeding: Apply continuous downward pressure on the manual feed handle before engaging auto-feed to "lock out" internal spindle sleeve gaps.
Temperature Compensation: Steel expands during cutting and shrinks by 0.01-0.03mm when cool. Always measure at ambient temperature or compensate by +0.02mm during machining.
Avoid "Stay-down" Retraction: Always keep the spindle rotating while retracting a reamer to prevent spiral scoring on the hole wall.
5. Troubleshooting Common Defects
| Problem | Likely Cause | Solution |
| Tapered Holes | Arm deflection/Spindle gap | Perform depth compensation; use pre-load technique. |
| Out-of-Roundness | Spindle runout/Chatter | Use floating holders; shorten tool overhang. |
| Positional Error | Incomplete locking | Follow the 3-step locking sequence; re-check with dial indicator. |
About Shanghai MFG Machinery Equipment Co., Ltd
At MFG Machinery, we specialize in precision machining solutions and high-performance tooling optimization. Whether you are looking to upgrade your workshop capabilities or require custom-engineered precision components, our team of experts is ready to assist.
Contact Us Today:
Website: www.mfg-machinery.com
Email: info@mfg-machinery.com
Address:Buildings 1-4, No. 408 South Yunzao Road, Baoshan District, Shanghai